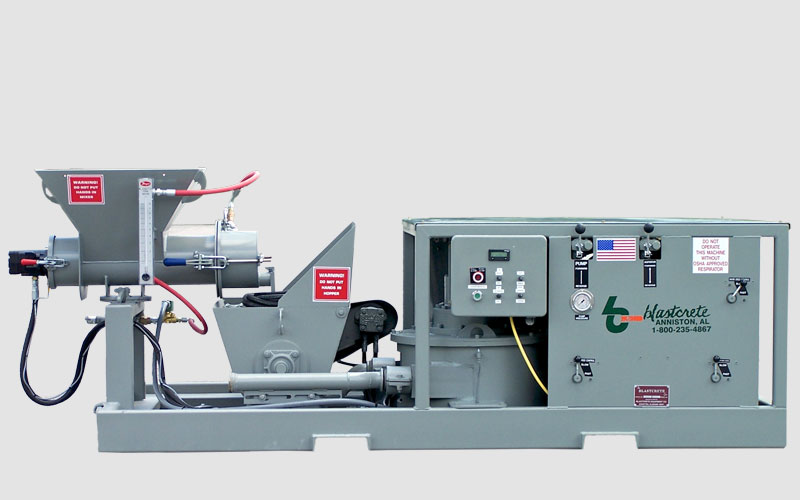
When choosing reliable pumping equipment for construction projects, long life pumping tubes are an important consideration for reducing maintenance requirements and supporting consistent operation. The Blastcrete MasonMate is designed to help contractors improve productivity in high-rise concrete masonry unit (CMU) block filling through its hydraulic squeeze pump, high-shear continuous mixer, and integrated bulk bag lifter.
Featuring a D3522 2-inch hydraulic squeeze pump driven by a heavy-duty planetary gearbox, the Blastcrete MasonMate is engineered for demanding masonry applications. The manufacturer highlights its long-lasting pumping tubes as a key advantage, helping contractors manage equipment maintenance while improving material placement efficiency.
Whether you are working on commercial buildings, high-rise masonry projects, or other suitable block-filling applications, the MasonMate combines pumping, mixing, and material handling in one compact machine.
What Are Long Life Pumping Tubes?
Long life pumping tubes are designed to withstand repeated use in pumping equipment while maintaining reliable material flow. In hydraulic squeeze pump systems, the pumping tube is a critical component that experiences repeated compression during operation.
Tube durability can influence maintenance frequency, replacement requirements, equipment downtime, and overall operating costs. Choosing a pumping system designed with durable tubes can help contractors improve equipment availability and manage long-term operating expenses.
The Blastcrete MasonMate incorporates a hydraulic squeeze pump and is promoted by the manufacturer for its long-lasting pumping tubes, making tube durability an important feature to consider when evaluating the machine.
Blastcrete MasonMate: Designed for Efficient Masonry Block Filling
The Blastcrete MasonMate is a labor-saving pumping and mixing system specifically designed for high-rise CMU block fill applications.
Traditional block filling can require workers to transport material manually using bucket brigades. The MasonMate helps eliminate this labor-intensive process by integrating material mixing, pumping, and bulk bag handling into a single machine.
According to the manufacturer, this system can reduce on-the-job labor by up to 75%. Its compact design also allows it to fit within a suitable freight elevator and operate in areas with ceilings as low as 8 feet.
By simplifying material handling and placement, the MasonMate helps contractors improve workflow and reduce unnecessary manual work.
Key Features of the Blastcrete MasonMate
1. Durable Pumping Tubes for Long-Term Use
The manufacturer identifies long-lasting pumping tubes as one of the MasonMate's key benefits. Tube durability is important in squeeze pump applications because the tube undergoes repeated compression during pumping.
Long-lasting tubes can help reduce the frequency of replacements and associated downtime. Actual tube service life depends on the material being pumped, operating pressure, maintenance practices, and working conditions.
2. D3522 Hydraulic Squeeze Pump
The MasonMate is equipped with a 2-inch D3522 hydraulic squeeze pump driven by a heavy-duty planetary gearbox.
The system is designed to support masonry block filling with a specified pumping pressure of 400 PSI and an output capacity of 0–6 cubic yards per hour.
Its hydraulic pumping design works alongside the continuous mixer to support an efficient material placement process.
3. High-Shear Continuous Mixer
The integrated high-shear continuous mixer helps prepare material for pumping. Combining mixing and pumping in one system can simplify operations and reduce interruptions caused by separate material preparation processes.
4. 1,000 lb. Capacity Bulk Bag Lifter
The built-in bulk bag lifter has a capacity of 1,000 pounds. This feature helps simplify material loading and reduce manual handling on construction sites.
5. Compact and Easy-to-Move Design
The MasonMate is designed to fit inside a suitable freight elevator and can be positioned using a telescoping forklift or crane. It is also designed to be moved with a pallet jack.
Its ability to operate under an 8-foot ceiling makes it suitable for selected high-rise and space-restricted construction environments.
6. Designed to Support Lower Operating Costs
Durable pumping tubes, integrated mixing, and labor-saving material handling can help contractors manage operating expenses. The manufacturer positions the MasonMate as a cost-effective pump to purchase, operate, and maintain.
Actual ownership costs depend on utilization, maintenance schedules, material compatibility, and job-site conditions.
Why Long Life Pumping Tubes Matter in Construction
For contractors using pumping equipment regularly, pumping tube durability can influence both productivity and maintenance planning.
Key benefits of durable pumping tubes include:
Reduced replacement frequency: Longer service life may reduce the need for frequent tube changes.
Long Life Pumping Tubes: Discover the Blastcrete MasonMate