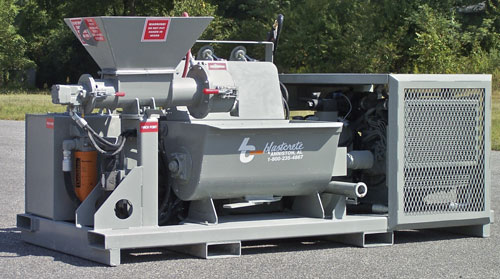
Choosing the right pump system for concrete masonry units (CMUs) is essential for improving construction productivity, reducing manual labor, and streamlining block-filling operations. The Blastcrete MasonMate is a specialized mixing and pumping system designed for high-rise CMU block filling, offering an efficient solution for commercial masonry contractors and construction professionals.
The Blastcrete MasonMate combines a D3522 hydraulic squeeze pump, a high-shear continuous mixer, and a 1,000 lb. capacity bulk bag lifter in one compact machine. Designed to eliminate traditional CMU block fill bucket brigades, the system can reduce on-the-job labor by up to 75%, according to the manufacturer.
For contractors working on multi-story buildings, commercial developments, and large masonry projects, the MasonMate helps simplify material handling, improve material placement efficiency, and support a more organized construction workflow.
Why Choose a Specialized Pump System for Concrete Masonry Units?
Concrete masonry unit filling requires a reliable method of preparing and delivering compatible fill material into block cavities. Traditional methods may involve separate mixing equipment and manual transportation, increasing labor requirements and slowing down construction.
A dedicated CMU pumping system combines important material preparation and placement functions to help improve workflow.
The Blastcrete MasonMate is designed specifically for high-rise block-filling applications. Its integrated components help reduce manual handling while supporting efficient material delivery.
Key advantages include:
Integrated hydraulic pumping and continuous mixing
A 1,000 lb. capacity bulk bag lifter
Reduced reliance on manual CMU block fill bucket brigades
Compact design for suitable high-rise construction sites
Pallet-jack mobility for easier positioning
Multiple power options for different job-site requirements
Long-lasting pumping tubes, as highlighted by the manufacturer
Blastcrete MasonMate: An Efficient CMU Block Filling Solution
The Blastcrete MasonMate brings pumping, mixing, and bulk material handling together in one system. This design helps contractors manage material preparation and delivery without relying on traditional manual bucket transportation.
The integrated high-shear continuous mixer prepares compatible material for pumping, while the D3522 hydraulic squeeze pump delivers it for block-filling applications. The bulk bag lifter supports material loading and helps reduce manual handling tasks.
According to the manufacturer, the MasonMate can reduce on-the-job labor by up to 75%. Actual labor savings depend on project layout, material requirements, crew size, and operating conditions.
The machine is also designed to fit within a suitable freight elevator or be positioned using a telescoping forklift or crane, making it worth considering for appropriate multi-story construction projects.
Key Features of the Blastcrete MasonMate
1. D3522 Hydraulic Squeeze Pump
The MasonMate features a 2-inch D3522 hydraulic squeeze pump driven by a heavy-duty planetary gearbox. It is designed to pump compatible materials for concrete masonry unit filling.
The specified pumping pressure is 400 PSI, with an output capacity of 0–6 cubic yards per hour.
2. High-Shear Continuous Mixer
The integrated high-shear continuous mixer helps prepare material for pumping. Combining mixing and pumping in one machine can simplify material preparation and reduce coordination between separate pieces of equipment.
This arrangement supports a streamlined workflow for suitable CMU block-filling operations.
3. 1,000 lb. Capacity Bulk Bag Lifter
The built-in bulk bag lifter has a stated capacity of 1,000 pounds. It supports material loading and can help reduce manual lifting requirements.
For contractors handling substantial quantities of dry material, this feature can simplify loading operations when used according to the manufacturer's instructions.
4. Compact Design for High-Rise Construction
Equipment access can be challenging on multi-story construction sites. The MasonMate is designed to fit within a suitable freight elevator and operate in spaces with ceilings as low as 8 feet.
The unit is also designed to move with a pallet jack and can be positioned using a telescoping forklift or crane.
Before transporting or lifting the machine, verify elevator dimensions, floor loading limits, access clearances, and approved lifting procedures.
5. Long-Lasting Pumping Tubes
The manufacturer highlights long-lasting pumping tubes as an important feature of the MasonMate. Durable pumping components can help contractors plan maintenance and manage replacement requirements.
Actual tube life depends on material characteristics, operating conditions, and maintenance practices.
6. Multiple Power Configurations
The Blastcrete MasonMate offers three listed power options:
Kubota water-cooled diesel engine
35 HP Briggs & Stratton gasoline engine
30 HP electric motor with starter and disconnect
Contractors can evaluate these options according to available site utilities, operating conditions, and project requirements. Confirm the selected configuration's availability and technical details with the supplier.
Blastcrete MasonMate Technical Specifications
The following specifications can help contractors determine whether this pump system for concrete masonry units meets their project requirements.
Specification Details
Pump type D3522 hydraulic squeeze pump
Pump size 2 inches
Pumping pressure 400 PSI
Output capacity 0–6 cubic yards per hour
Discharge 2-inch heavy-duty
Hopper capacity 3 cubic feet
Dimensions 90 × 44 × 72 inches
Machine weight 2,600 lbs.
Bulk bag lifter capacity 1,000 lbs.
Operating clearance Designed for an 8-foot ceiling
Power options Diesel, gasoline, or electric
Dimensions are specified with the bag lifter in the charging position. Confirm final specifications and configuration details with the manufacturer.
Benefits of Using a CMU Pumping System
Reduced Manual Labor
The MasonMate helps eliminate traditional CMU block fill bucket brigades. According to the manufacturer, this can reduce on-the-job labor by up to 75%, depending on project conditions and workflow.
Improved Material Placement Efficiency
The integrated mixer and hydraulic squeeze pump help streamline material preparation and delivery, supporting a more organized block-filling process.
Simplified Material Handling
The 1,000 lb. capacity bulk bag lifter supports loading and can reduce manual material handling tasks.
Better Space Utilization
Its compact dimensions, pallet-jack mobility, and freight-elevator compatibility make the MasonMate worth evaluating for suitable high-rise projects with restricted access.
Potential Operating Cost
Pump System for Concrete Masonry Units: Discover the Blastcrete MasonMate